One-stop solution for Sheet Metal Fabrication & CNC Machining - Bergek CNC
Language
One-stop solution for Sheet Metal Fabrication & CNC Machining - Bergek CNC
Recently, I introduced a lot of knowledge about sheet metal bending processing. Today, I will continue to talk to you about what problems need to be paid attention to in the sheet metal bending processing and forming process. The following five aspects are summarized.
CNC sheet metal bending delivers unparalleled precision and quality, ensuring that every bend meets exacting specifications and maintains structural integrity. With advanced processing techniques, such as the creation of semicircles and R angles, this method minimizes material deformation and enhances durability, tailored to various thicknesses and shapes. Coupled with a robust quality control system and flexible production capabilities, our service guarantees consistent results that align with customer requirements, making CNC sheet metal bending an ideal choice for a wide range of applications.
**Team Strength**
Our Expert CNC Sheet Metal Bending team combines experience and innovation, ensuring precision and quality at every stage of production. Our skilled engineers and technicians bring decades of expertise, utilizing state-of-the-art technology to meet the highest standards. Collaboration is at the heart of our operations, fostering a culture of continuous improvement that drives unparalleled craftsmanship. Each team member is committed to understanding your unique needs, ensuring tailored solutions that enhance efficiency and reduce lead times. With our dedicated professionals, you can trust that your projects are in capable hands, delivering exceptional results that stand the test of time.
**Team Strength**
At the heart of our Expert CNC Sheet Metal Bending service is a dedicated team of skilled artisans and engineers, each passionate about delivering precision and quality. Our team combines years of expertise in CNC technology with advanced training in sheet metal fabrication, ensuring every project meets the highest standards. We pride ourselves on our collaborative approach, where creativity meets craftsmanship. This synergy drives innovation, allowing us to tackle complex design challenges efficiently. With a commitment to continuous improvement and customer satisfaction, our team's strength lies not only in their technical skills but also in their unwavering dedication to excellence in every bend and contour.
What are the bending forming process details of sheet metal bending processing?
Recently, I introduced a lot of knowledge about sheet metal bending processing. Today, I will continue to talk to you about what problems need to be paid attention to in the sheet metal bending processing and forming process. The following five aspects are summarized.
Do the semicircle. Make a semicircle on both sides of the bending line first, which can prevent the sheet metal from protruding due to extrusion on both sides of the bending Angle after bending. Convex size and sheet metal thickness, the thicker the material, the more convex, therefore, the diameter of the semicircle are better than 1.5 times the thickness of the material.
Do R Angle. If you do not make R Angle, after many times of stamping, the original right Angle will gradually disappear to form R Angle, but at this time, one side or both sides of R Angle will have a little side length. Therefore, make R Angle before bending, and the Angle inside should be greater than or equal to half of the material thickness. If there is no clear requirement a right Angle, should be processed into an R Angle; In the process of drawing, R Angle should be marked to avoid damage to the mold when the line is stopped.
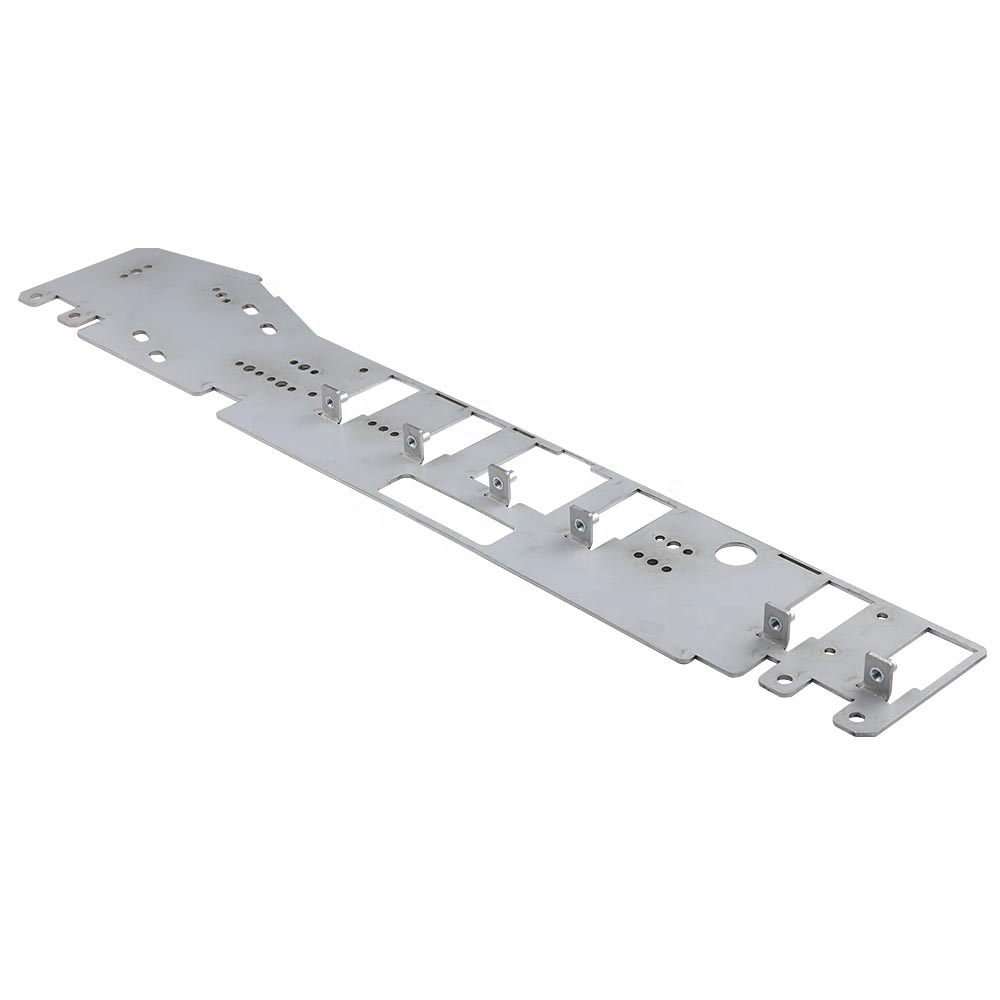
Make a narrow or open side hole. In order to avoid rough edges, it is necessary to make a narrow hole or edge hole at the turning point between the plane and the bending surface, and the width of the narrow hole should be greater than or equal to 1.5 times the thickness of the meat.
A discount. The discount edge is divided into unilateral and bilateral, compared with unilateral discount, the bilateral discount is more accurate, and the height of the discount edge is greater than 3mm; The parts on the side wall are required to be more than 10mm from the bottom surface; There are side wall opening can not be too close to the bottom surface, to keep above 3mm, otherwise the hole will be deformed by pressure.
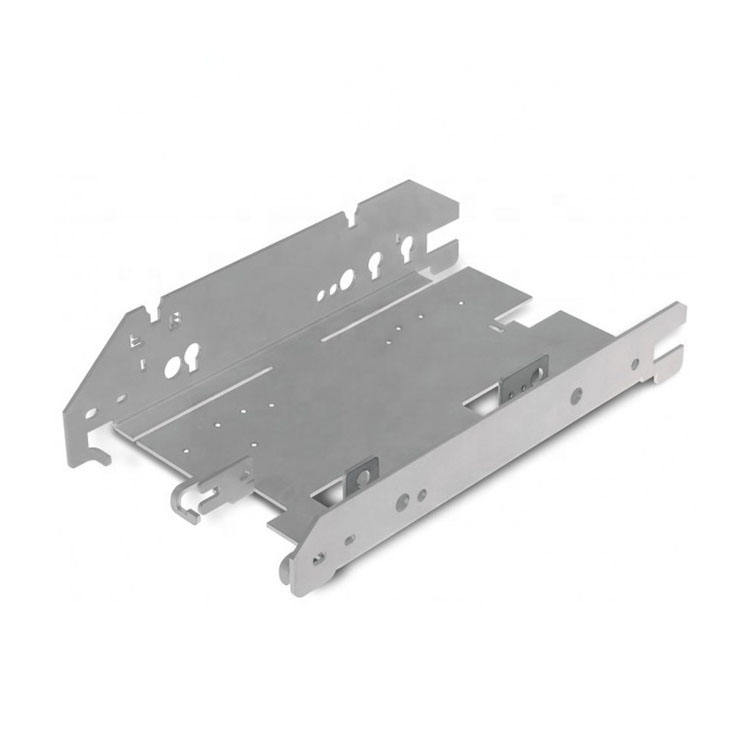
It should be deformed after bending. There are two cases of deformation. First, in view of the deformation formed by the force after bending, without affecting other parts, can be added in the bending Angle of 45 degrees of reinforcing additives, increase the strength; Two, because the plate shape is long and narrow type is not easy to keep straight, bending deformation, which can be folded an L or folded two inverted "U" type edge, but sometimes will be interrupted by some factors, can not connect from head to tail, then you can play the right amount of convex ribs to increase its strength.
Bending processing molding
The above is to give you a summary of the bending molding process need to pay attention to the aspects, I hope to help you. Bergek processing plant with experience to tell you the small details of sheet metal bending process, so that you can avoid mistakes in the process of operation, but also in strict accordance with customer requirements drawings for processing.
Bergek CNC is a world-class manufacturing service provider in Shenzhen. We have advanced equipment to provide a full range of customized products to manufacturers around the world, specializing in CNC machining and sheet metal processing.
If you have any question,please contact us.
Copyright © 2026 SHENZHEN BERGEK TECHNOLOGY CO., LTD. - www.bergekcnc.com All Rights Reserved.